3D scanning · EinScan Rigil
Scan your part into a 3D file
Receive an STL, a CAD model or a comparison with the design. We scan small brackets and complete machines.
- Specification for 100 mm
- 0.046 mm
- Specification for 1 m
- 0.100 mm
Manufacturer's Laser HD data; not a measurement of your part or a printed-part tolerance.
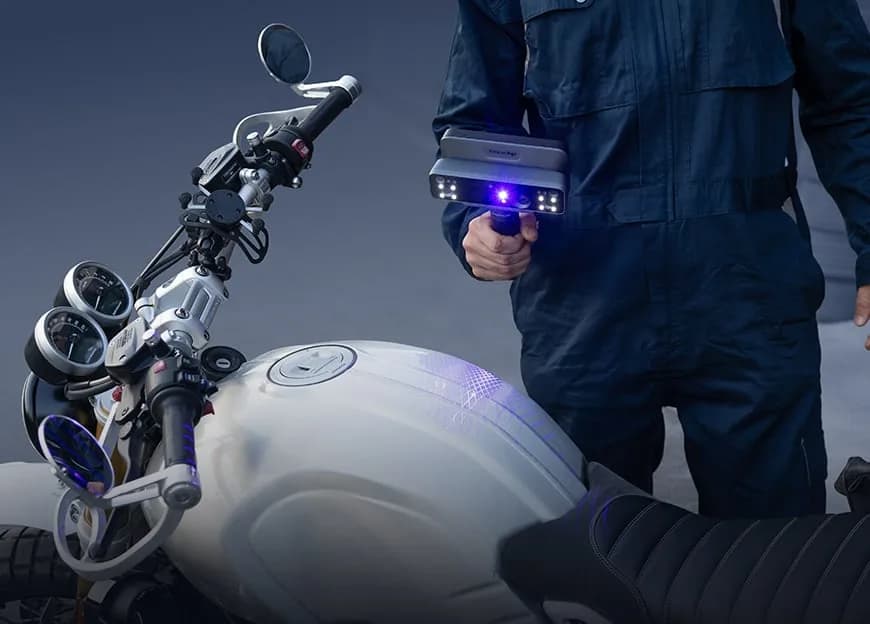
- 0.046 mm · specification for 100 mm
- resolution setting 0.05 mm
- STL · STEP · report
What you get: choose the deliverable
Net prices
STL · OBJ · PLY
Mesh
Records accessible surfaces in their current condition, including wear. A mesh can be edited, but has no operation history or dimensions from a parametric CAD model.
For documentation, for measurement, for archiving a shape that is not on the drawing.
from PLN 250.00
Quote a meshSTEP · native CAD
Solid model
Reconstructs geometry using scans, measurements and available documentation. We agree critical dimensions and assumptions; a parametric model is created where possible.
For part production, for design changes, for handover to the tooling department.
from PLN 350.00
Quote a CAD modelPDF · color map
Deviation report
Comparison with supplied CAD: a deviation map on scanned surfaces and agreed sections. We agree inspection scope and alignment datums before work; unseen areas remain outside measurement.
For batch evaluation from a supplier, for claims, for the first piece from a mold.
price on request
Quote a deviation report
PLN amounts are domestic starting prices, net of VAT. Export orders require an individual quotation. We confirm the final scope and price after reviewing the part and requirements.
CAD reconstruction is also part of the reverse-engineering process. We agree modelling scope before work; printing is quoted separately.
Scan accuracy by part size
Shining3D, EinScan Rigil
The manufacturer's Laser HD volumetric accuracy specification is 0.04 mm + 0.06 mm/m. The table gives the formula value for each size, rather than the measured error of a particular scan. Surface, access and data alignment affect the result.
Scroll the table sideways to see the remaining columns.
| Part dimensions | Specification value | Example |
|---|---|---|
| 100 mm | 0.046 mm | Support, gear wheel, knob. |
| 300 mm | 0.058 mm | Housing, guard, cover. |
| 500 mm | 0.070 mm | Body element, tank, gearbox housing. |
| 1000 mm | 0.100 mm | Frame, tabletop, control cabinet doors. |
| 2000 mm | 0.160 mm | Entire machine or workstation, in the context of assembly. |
Accuracy ≠ Resolution
The finest published Laser HD resolution setting is 0.05 mm. It describes data density; it does not guarantee capture of a feature that size or dimensional accuracy.
Accuracy ≠ Part Tolerance
Drawing and part function define tolerance. Reconstruction, printing and measurement conditions affect the result; critical fits are checked on a trial piece. We explain this in a separate article.
Scanning different surfaces
The scanner looks at reflected light
Usually without spray
Matte plastic, rubber, sintered material, casting
Usually permits scanning without spray. We check stability and tracking; soft rubber must not change shape during measurement.
Usually without spray
Machined metal, paint coating
We assess reflections and data coverage. Laser HD can scan metal without spray, but gloss, shape and access need checking.
Preparation assessment
Transparent and mirror surface
May require scanning spray. We agree preparation and permission before use; do not apply a matt coating yourself.
Preparation assessment
Deep matte black
Black colour alone does not determine spray use. We first assess the reading and reflections; any preparation is agreed with the owner.
Select the method
Enclosed interiors, channels, deep holes
Optical scanning captures surfaces visible to the scanner. Closed interiors and inaccessible hole bottoms need another method; we do not promise to capture them.
Select the method
Small and prismatic detail
Manual measurement often suffices for simple dimensions. We select the method for geometry and requirements; a small part is not automatically excluded from scanning.
From detail to file
Four steps
01 · ACCEPTANCE
Part or on-site visit
The part arrives by courier. A machine standing on the line cannot be shipped, so in that case we travel, and we quote the trip separately.
02 · PREPARATION
Surface preparation and markers
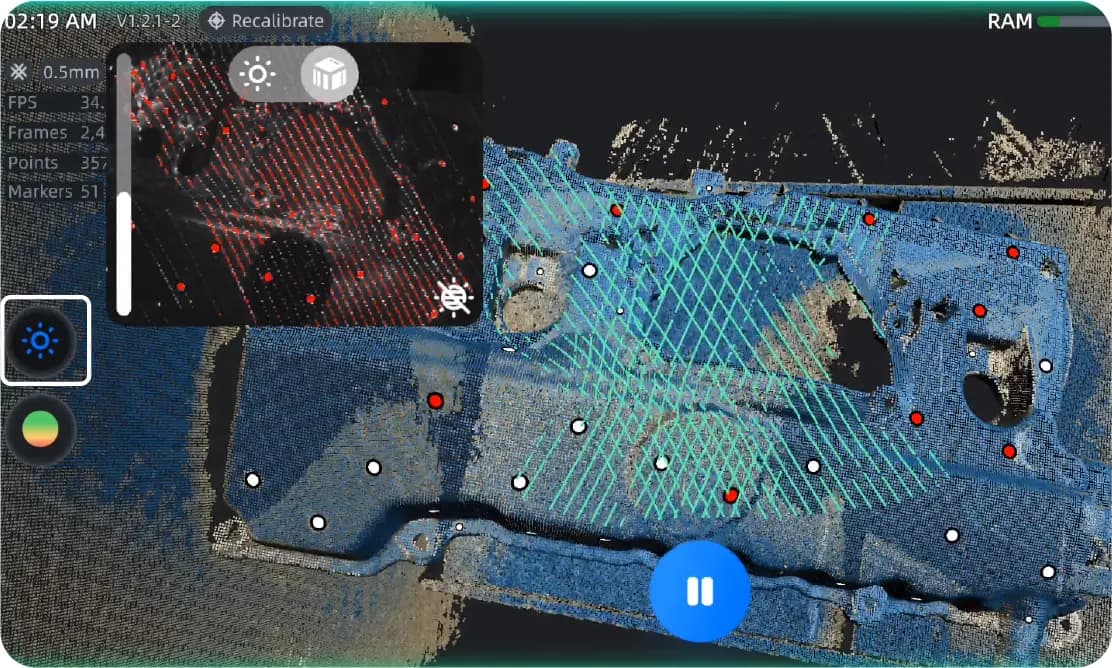
We check the surface and tracking stability. Markers or spray are selected for the part; their use is agreed before preparation.
03 · SCAN
Laser HD, several settings
For part reconstruction we use Laser HD from several sides. We align accessible surfaces and check coverage; the mode alone does not guarantee a result for every part.
04 · MESH
Cleaning and export
Remove background and noise, export STL, OBJ or PLY. Filling gaps is reconstruction rather than measurement; its scope and a CAD model are agreed separately.
A handheld scanner has no printer build chamber. We assess size and access before travelling; separately we check whether the model can be printed in one piece, split or made using another method.
EinScan Rigil, Shining3D
Manufacturer data
Laser HD
Blue laser, 25+25 crossed lines. For reconstructing part geometry. The accuracy and resolution data published here apply to this mode.
VCSEL Infrared
Wider scanning coverage; alignment using features, texture or markers. For larger objects and assembly context. It has a separate specification; Laser HD data does not apply to it.
- Laser HD volumetric accuracy
- 0.04 mm + 0.06 mm/m
- Finest Laser HD setting
- 0.05 mm
- crossed lines
- 25+25
- working distance, mm
- 170–550
Source: Shining3D: EinScan Rigil specification. Other equipment: machines in Olsztyn.
What the scan cannot do
Before you send the part
- We do not issue calibration certificates. A scan report compares geometry; it is not a coordinate-measuring-machine report.
- We do not reproduce trademarks or styling. Replacement-part reconstruction excludes the manufacturer's logo.
- We do not read tolerances or fits. The scan shows the dimension of the worn part, not the designer's intent.
- We do not recognize the material. We assess the type based on appearance and behavior; we do not perform composition analysis.
- We cannot restore a dimension that wear has erased without a trace. We will inform you of this before starting work.
Submitted files are kept privately and remain available for quotation and production for 90 days from the enquiry. After that, they are unavailable for repeat orders and scheduled for deletion. We can sign a confidentiality agreement before you send the part.
What file do you need from the scan?
Send photos, part dimensions and the required output: a mesh, a CAD model or a deviation report. We will confirm the scope and cost after reviewing them.
Describe the scan I need a finished partQuick contact
Discuss the part before shipping
Leave a phone number or email. We will discuss the scan scope, part delivery and file confidentiality.
Loading the form details. Please wait a moment.